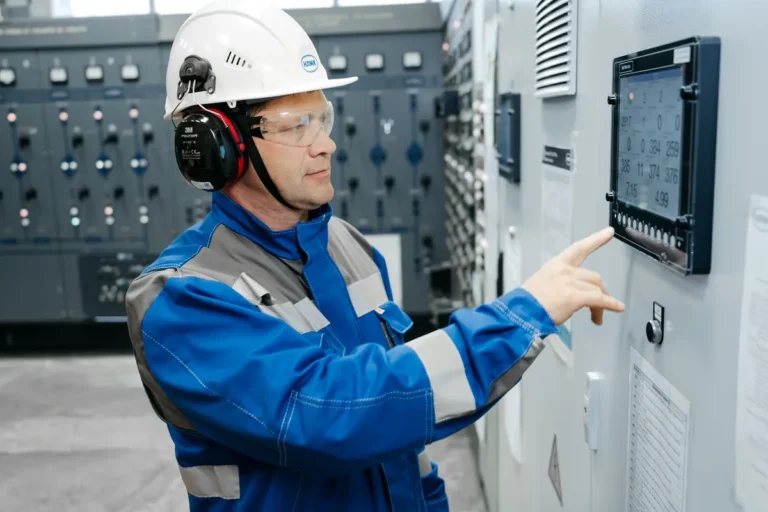
A shrink wrap machine factory acceptance test should produce traceable evidence that the contracted machine meets agreed requirements before shipment. An informal demonstration is not a FAT. Freeze the protocol
A shrink wrap machine factory acceptance test should produce traceable evidence that the contracted machine meets agreed requirements before shipment. An informal demonstration is not a FAT. Freeze the protocol
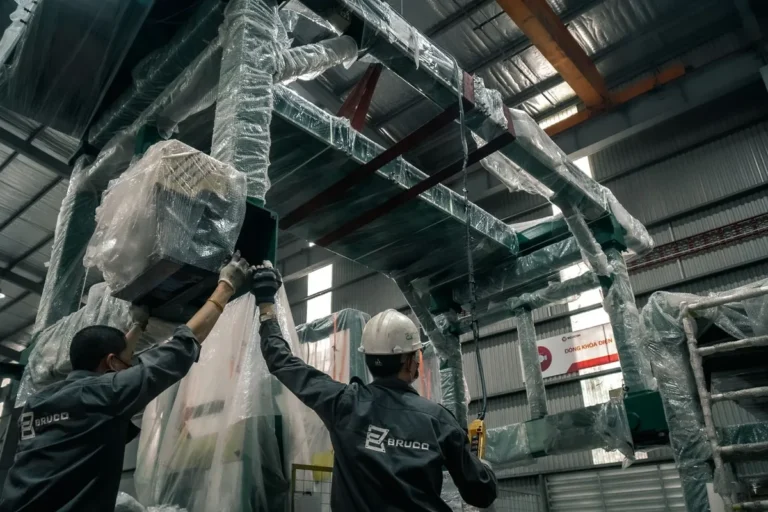
Shrink wrap machine installation should not be scheduled until the receiving site has passed a documented readiness review. Before the equipment ships, confirm the delivery route, approved layout, floor conditions,
A shrink wrap machine RFQ should define the product range, finished package, film, sustainable output, operator boundary, site utilities, line interfaces and acceptance test. Sending only “automatic shrink wrapper” invites
Shrink wrap machine ROI must compare the cash flow of a measured baseline with the cash flow expected from the proposed process. Use the same cost boundary for both cases,
Rigid boxes, printed materials, trays, bottles, cans, cartons and grouped industrial products are candidates for shrink wrapping when the complete product tolerates the validated sealing, thermal and compression conditions. Suitability
Shrink wrap defects are evidence, not diagnoses. Their location, the first process stage where they appear, whether they repeat in the same place, and what changed since the last accepted
Shrink tunnel temperature is one input to a thermal-exposure process. Conveyor speed sets residence time, airflow moves heat around the package, and product spacing and load pattern affect how that
Shrink wrap sealing temperature is not a universal number and may not be a directly adjustable parameter on every sealing architecture. The displayed setting, actual condition at the film interface,
Choose shrink film gauge and width as part of one film specification. Width must cover the product through the actual film path and leave the sealing allowance required by the
Shrink wrap machine speed should be specified as accepted packages produced over a defined period and SKU mix. A maximum cycle figure is not the same as sustainable throughput. Product