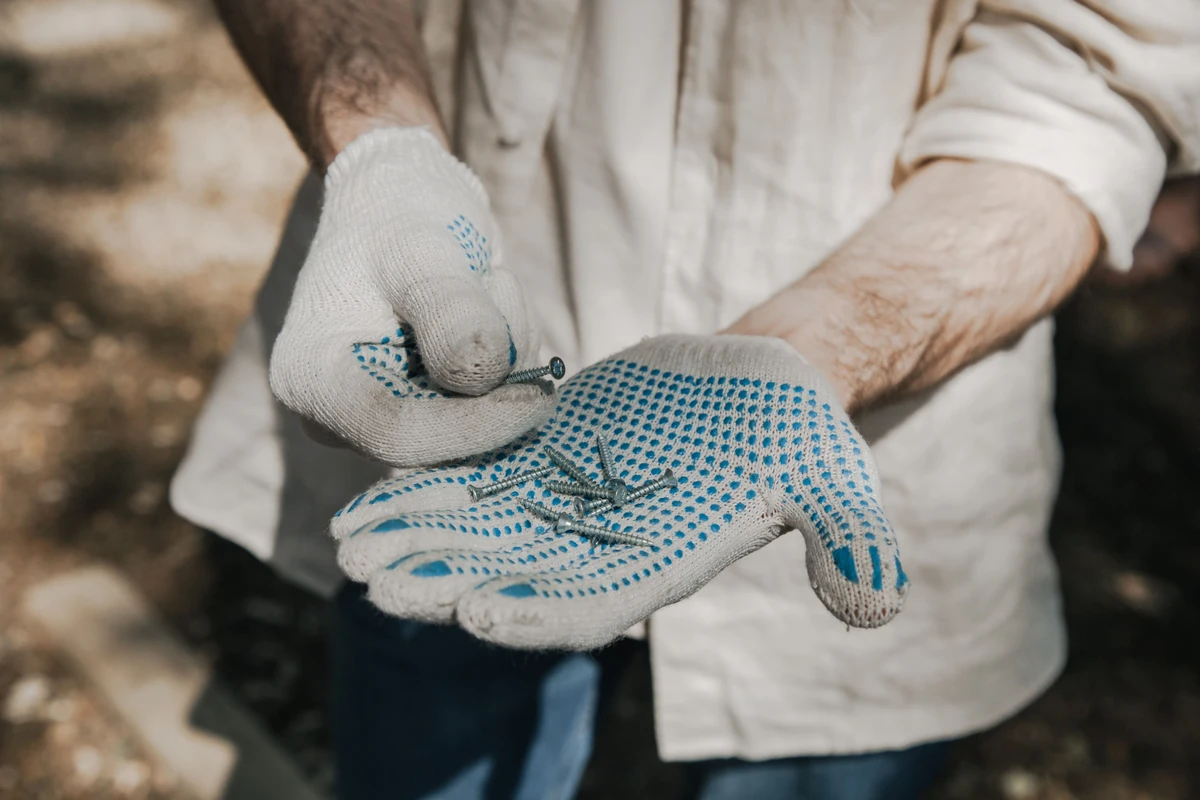
Hardware kit packaging needs three separate checks: the correct component, the approved revision, and the required quantity. A sealed bag proves that the sealing step has finished; it does not prove that every screw, washer, bracket, or instruction sheet inside belongs to the kit.
Build the packing process around an approved bill of materials, then assign a check to each credible error. Keep component confirmation separate from bag feeding and sealing. A manually loaded auto bagger is a useful option when the team wants to mechanize bag handling while retaining control of kit assembly and inspection.
The practical buying question is therefore: Can this station load, check, identify, and seal the actual kit through a repeatable sequence? Answer that question with representative components and bags before selecting counting accessories or increasing output.
Start Hardware Kit Packaging with One Approved Kit Definition
The kit definition must identify what belongs in one finished pack, including its version. A product name such as “mounting kit” is too broad when different customers, assemblies, or revision levels use similar components.
Use the released bill of materials, or BOM, as the reference. Record the kit number, revision, component numbers, quantities, permitted substitutions, and required inserts. Include packaging and identification requirements in the work instruction so that the team does not assemble the correct parts into an incorrectly identified bag.
Distinguish a component revision from a supplier batch. A batch identifies a source or production lot; a revision identifies the approved design or specification. The packing record needs whichever information the customer requires, without treating one as a substitute for the other.
Where an approved substitute exists, make that permission visible at the station. Operators should not decide that two similar screws or brackets are interchangeable because both fit into the bag.
Turn the BOM into a Component Control Table
Assign a confirmation method to each component rather than relying on a final glance at a mixed pile. The table below is a hypothetical assembly-kit example, not a SelectPack customer specification.
| Component | Per kit | Main error to catch | Confirmation point |
|---|---|---|---|
| Screw S-A, approved revision | 4 | Similar screw from another kit | Verify source bin and count |
| Nut N-A | 4 | Missing or extra nut | Confirm quantity before loading |
| Washer W-A | 8 | Nested washers counted as one | Separate and verify pieces |
| Instruction insert I-A, current revision | 1 | Old insert or missing sheet | Check identifier before loading |
Add the responsible role and evidence to the site’s actual table. Evidence might be an operator confirmation, an inspected tray, a validated counting result, or another method specified in the control plan.
Keep source containers identifiable while parts are transferred. If a supplier carton holds several inner packs or batches, document the level at which identity is confirmed. An unlabelled replenishment container breaks the connection between the approved BOM and the parts reaching the bagger.
For similar parts, use the discriminating feature: length, thread, finish, hole pattern, drawing revision, or a controlled identifier. A generic description such as “silver screw” will not support a reliable check where several silver screws share the station.
Which Checks Establish Identity and Which Establish Quantity?
A quantity check establishes how many items are present under its validated conditions. It does not automatically establish that those items are the correct part or revision.
A tray with four positions can help an operator organize four pieces, but four occupied positions still need the correct screw. Likewise, a counter’s displayed total does not confirm the identity of material placed into its input. Source verification remains a separate task unless the quoted system explicitly provides and validates that function.
Total-weight checking also needs a defined detection scope. Similar-weight substitutions, variation between components, and changes in the bag or insert affect the result. Establish which missing, extra, and wrong-component conditions the proposed method detects with the real kit. Do not buy a scale on the assumption that a passing weight proves every BOM line is correct.
Prepare controlled challenge samples outside saleable production: a missing washer, an extra nut, the wrong screw, and the old insert. Compare the inspection result with the known contents. Identify each challenge pack clearly and reconcile it after testing so that it cannot enter customer shipments.
Set inspection frequency and release responsibility through the site’s quality plan. This guide does not prescribe a universal sampling rate or detection threshold.
Place the Confirmation Point Before the Bag Closes
Verify loose components while the team can still identify and separate them. Once hardware overlaps inside a filled bag, visual checking becomes more difficult and correcting a kit requires additional handling.
For a manually loaded station, a workable sequence is to confirm source identity, assemble one kit in a defined preparation area, check its contents, and transfer that kit into the presented bag. Keep unchecked material, confirmed kits, and finished bags in distinct locations. The purpose is to make the status of each pack visible without relying on memory.
The transfer itself deserves attention. Small washers can remain in a tray; components can bridge at the bag mouth; an insert can be left beside the machine. Inspect the actual transfer path and define how the operator confirms that the checked kit has reached the bag before sealing.
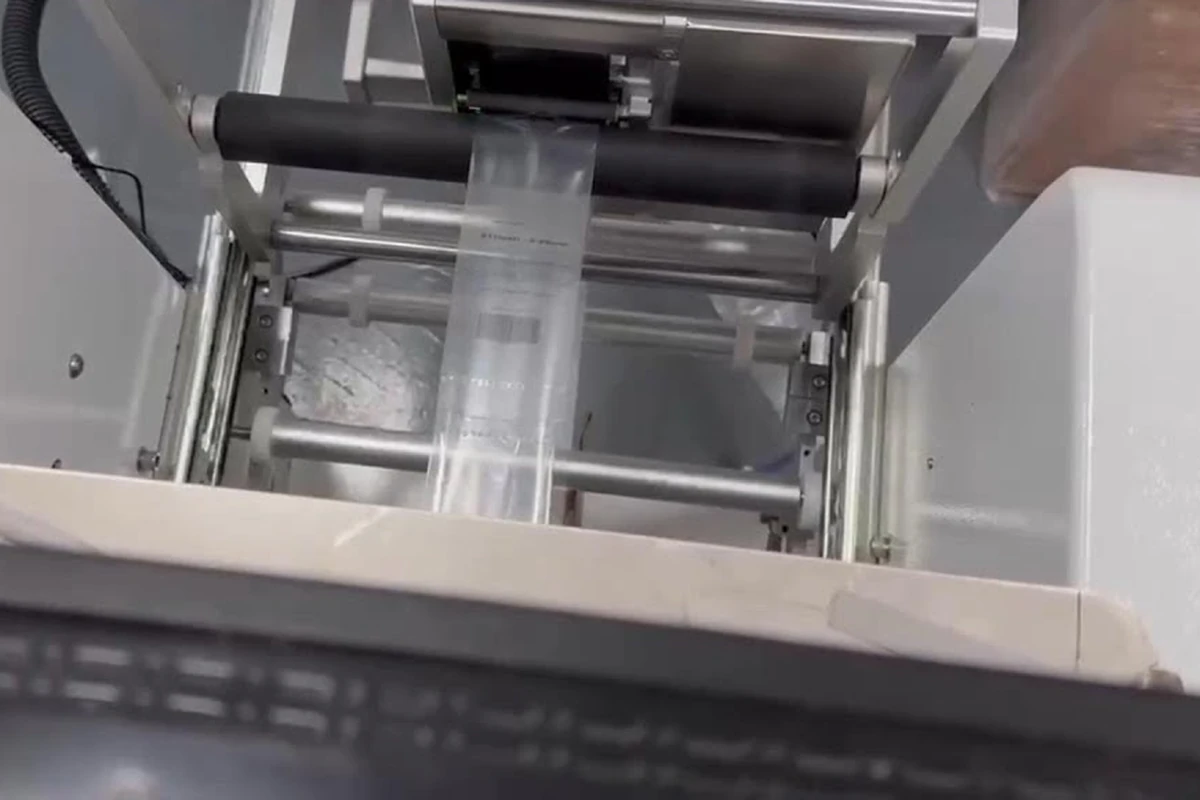
Bag fit also affects that sequence. Leave the clearance required for loading and sealing, and evaluate puncture risk from sharp threads or edges. The pre-opened bags-on-a-roll guide provides the broader bag-selection context; compatibility and the final pack still require confirmation for the exact machine and hardware.
Keep the Kit ID Attached to the Correct Contents
Product identification needs its own confirmation even when component inspection has passed. A complete kit in a bag marked with another kit number is still an incorrect shipment.
Match the printed or applied identifier to the active kit definition. Confirm the required revision, customer reference, batch information, and any variable fields using the approved source. Direct printing is a configuration choice, not proof that the selected data is correct.
Where scanning is used, distinguish reading a code from verifying its association with the contents. The auto bagger barcode verification guide explains how to check expected data, decoded data, and the physical pack separately.
Control this association during material replenishment and job changes, not only at the beginning of a shift. Use a bagging machine changeover checklist to remove previous-job components, bag stock, and identifiers before releasing the next kit.
What Happens to an Incomplete or Uncertain Kit?
An incomplete or uncertain kit goes to a defined hold area until its status is resolved. Returning an unidentified handful of parts to the active bin can transfer the same uncertainty to subsequent packs.
Record the kit number, observed problem, source material involved, and the range of packs requiring review. Keep correction and release separate: adding a missing component is a rework action; confirming the corrected kit against its BOM is the release check.
For sealed rejects, use the site’s approved unpacking and reinspection process. Account for damaged bags and identifiers, and confirm that the corrected pack receives the appropriate identification. Repeated missing-component failures should trigger a review of the preparation and transfer steps, rather than repeated recounting at the end of the line.
Specify the Bagger around the Complete Kit Process
Send SelectPack a complete representative kit, its BOM and revision, the intended bag, and the defects that the inspection method must detect. Add product dimensions, sharp-edge concerns, expected batches, required identifiers, and the proposed operator sequence.
Discuss bag presentation, loading access, sealing, and identification against that sequence. Counting, weighing, vision inspection, scanner interlocks, and automatic rejection are separate configuration requirements; request written confirmation of the functions actually included and the conditions under which they have been tested.
Use the SelectPack auto bagging machine range to start that application review. A useful trial follows a complete, correctly identified kit through checking, transfer, and sealing.